
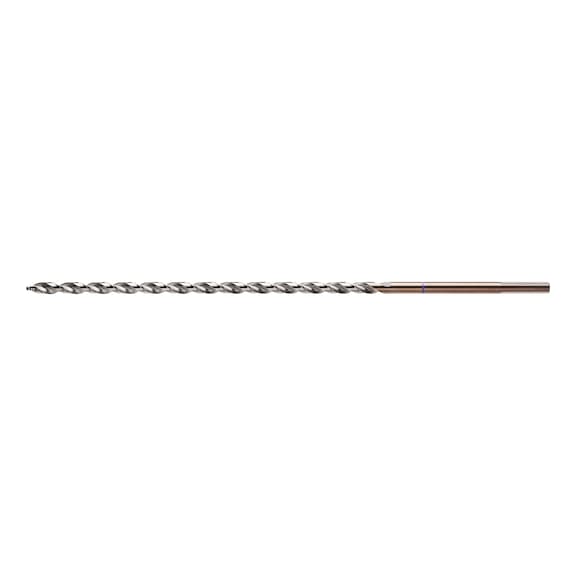






SMART STEP EU+ HSCo twist drill bit DIN 1869 R2
DRL-MET-DIN1869-HSCO-SMARTSTEP-D4,0
Art.-no. 0626960400
EAN 4068362001642


Register now and access more than 125,000 products
Advantages of the SMART STEP drill bit tip geometry with extremely uneven pitch (EU+)
- Up to 50 % longer service life
- Significantly more comfortable drilling with less vibration, even less effort and perfect tool guidance (up to 60 % less torque)
- Up to 20 % lower energy consumption
- Up to 15 % faster drilling progress
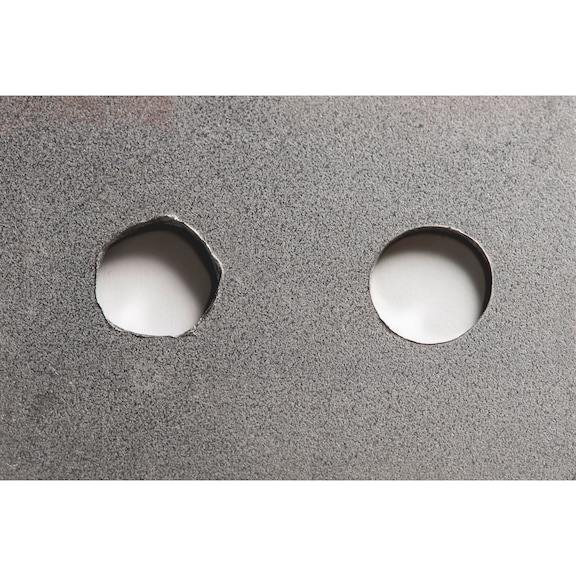
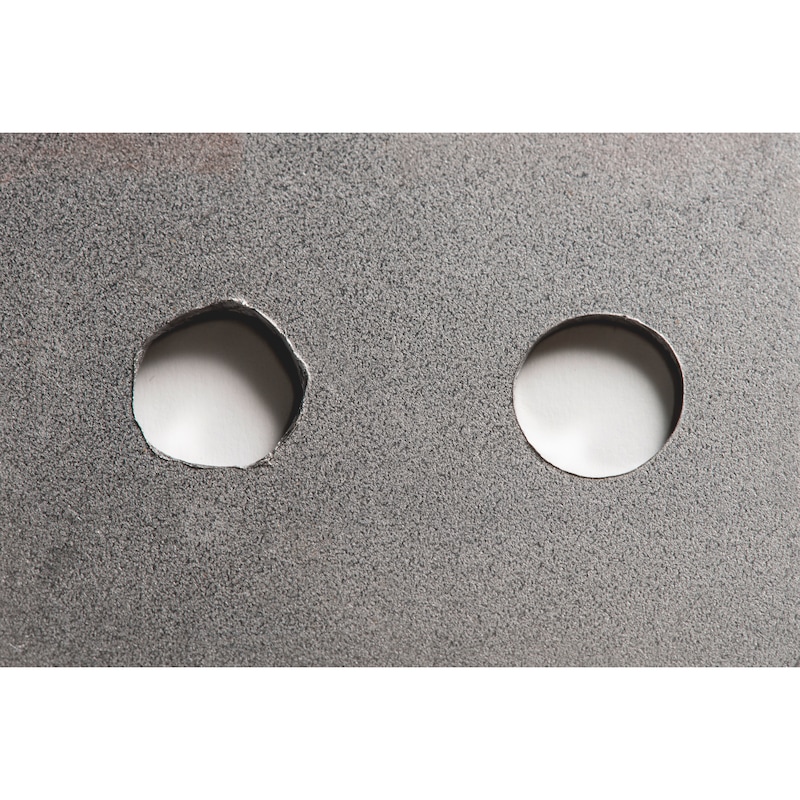
Precise, circular drill holes in almost all materials
- Very precise drilling without tearing or splintering the material
Very comfortable drilling
- No pre-drilling required despite the extra-long design
- The tool does not run off-centre even when drilling particularly deep holes
- Simple drilling or enlarging of an existing drill hole
- No rattling or catching, even in thin-walled materials
- Burr-free hole exit
Very fast drilling
- Significantly faster and with less effort required compared to extra-long HSCo twist drill bits with conventional tip geometry
3-flat shank
- No spinning in the drill chuck: Faster, more comfortable working
- Optimal power transmission
- Protects the drill chuck from damage
- Little effort required to loosen and tighten the drill chuck
Available exclusively from WÜRTH
Product packaging made from 100 % PCR (recycled plastic from household waste) and 100 % recyclable
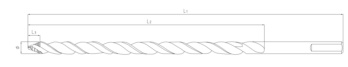
- For blind holes, please be aware of the extended drill tip (see dimension l3)!
- The innovative tip geometry drills step by step to achieve the required diameter. During the drilling process, multiple main cutting edges break up the chip into small individual chips for optimal chip removal. This ensures highly precise, circular drill holes.
- The simultaneous use of several cutting edges ensures very fast, comfortable working and a long service life.
- The service life can be significantly increased by using sufficient coolant and lubricant. This is strongly recommended especially when drilling stainless steel.
Datasheets(X)

- Ideal for use in cordless drivers as well as on hand-held, box column and pillar drills
- For universal use in almost all materials, such as stainless steel (e.g. V2A, V4A), heat-resistant steels and titanium. Also for general applications in conventional steel up to 1,300 N/mm², as well as in cast iron, aluminium, plastic, non-ferrous metals, compact and hard wood and soft and light wood.
- Significantly longer service life than long wood twist drill bits when drilling in wood.
To achieve optimum drilling progress and avoid jamming, frequent "ventilation" of the drill bit is required for large drilling depths.
 | |
Suitable for machine type | Drill, Cordless screwdrivers, Pedestal drilling machine |
Material to be processed | Steel, Cast iron, Stainless steel, Titanium, Non-ferrous metal, Wood, Hardwood |
Quality | ZEBRA-Premium |
Standard / drilling depth | DIN 1869 / 25xD |
Design | Extra long |
Diameter (Ø) | 4.0 mm |
Length (l1) | 220 mm |
Chip flute length (l2) | 150 mm |
Drill tip length (l3) | 2.55 mm |
Shank diameter | 4.0 mm |
Shank style | 3-face shank |
Surface | Oxide finish |
Cutting material | HSCo |
Service life (points system) | 3 of 4 points |
Drilling speed (point system) | 4 of 4 points |
Bore hole quality (point system) ( ) | 4 of 4 points |
Versatility (points system) | 4 of 4 points |
Drilling behaviour (point system) | 4 of 4 points |
Suitable for drill (points system) | 4 of 4 points |
Suitable for cordless drills (points system) | 4 of 4 points |
Suitable for upright drilling machine (points system) | 4 of 4 points |
Self-centring | Yes |
Suitable for tensile strength up to | 1300 N/mm² |
Material of sub-group | General structural steels, Non-alloyed tempering steels, Nitriding steels, Tool steels, High-speed steels, Cast iron, Ductile iron, Malleable cast iron, White cast iron, Stainless steels, sulphurated, Stainless steels, martensitic, Stainless steels, austenitic, Titanium, Titanium alloys, Spring steels, Aluminium, Aluminium alloys, Aluminium casting alloys (<10% silicon), Magnesium alloys, Copper, low-alloyed, Brass, short-chipping, Brass, long-chipping, Bronze, short-chipping, Bronze, long-chipping, Plastics, thermoset, Plastics, thermoplastic |
| Cutting values for SMART STEP EU+ HSCo DIN 338 twist drill bit | ||||||||||||
| For dia. 1.0-2.5 | ||||||||||||
| Material designation | Tensile strength | from dia. 1.0 | from dia. 2.0 | from dia. 2.5 | ||||||||
| vc | n | f | n | f | n | f | ||||||
| from | to | from | to | from | to | from | to | |||||
| General structural steels | ≤ 850 N/mm² | 18 | 27 | 5732 | 8598 | 0,01 | 2866 | 4299 | 0,012 | 2292 | 3439 | 0,015 |
| Unalloyed hardened steels | ≤ 850 N/mm² | 18 | 27 | 5732 | 8598 | 0,01 | 2866 | 4299 | 0,012 | 2292 | 3439 | 0,015 |
| Low-alloy hardened steels | ≤ 850 N/mm² | 18 | 27 | 5732 | 8598 | 0,01 | 2866 | 4299 | 0,012 | 2292 | 3439 | 0,015 |
| Unalloyed hardened steels | ≤ 1,000 N/mm² | 15 | 23 | 4777 | 7324 | 0,008 | 2388 | 3662 | 0,01 | 1910 | 2929 | 0,012 |
| Low-alloy hardened steels | ≤ 1,000 N/mm² | 15 | 23 | 4777 | 7324 | 0,008 | 2388 | 3662 | 0,01 | 1910 | 2929 | 0,012 |
| Alloyed hardened steels | ≤ 1,300 N/mm² | 10 | 15 | 3184 | 4777 | 0,008 | 1592 | 2388 | 0,01 | 1273 | 1910 | 0,012 |
| Nitriding steels | ≤ 1,300 N/mm² | 10 | 15 | 3184 | 4777 | 0,008 | 1592 | 2388 | 0,01 | 1273 | 1910 | 0,012 |
| Tool steels | ≤ 1,300 N/mm² | 10 | 15 | 3184 | 4777 | 0,008 | 1592 | 2388 | 0,01 | 1273 | 1910 | 0,012 |
| High-speed steels | ≤ 1,300 N/mm² | 10 | 15 | 3184 | 4777 | 0,008 | 1592 | 2388 | 0,01 | 1273 | 1910 | 0,012 |
| Cast iron | ≤ 350 HB | 15 | 23 | 4777 | 7324 | 0,008 | 2388 | 3662 | 0,01 | 1910 | 2929 | 0,012 |
| Spheroidal graphite and malleable iron | ≤ 350 HB | 15 | 23 | 4777 | 7324 | 0,008 | 2388 | 3662 | 0,01 | 1910 | 2929 | 0,012 |
| Stainless steels | 1,300 N/mm² | 8 | 12 | 2547 | 3821 | 0,01 | 1273 | 1910 | 0,012 | 1019 | 1518 | 0,014 |
| Titanium | 850 N/mm² | 6 | 10 | 1910 | 3183 | 0,008 | 955 | 1592 | 0,01 | 764 | 1273 | 0,012 |
| Aluminium | ≤ 600 N/mm² | 35 | 45 | 11146 | 14331 | 0,01 | 5573 | 7165 | 0,012 | 4458 | 5732 | 0,015 |
| Thermosetting plastics | 15 | 23 | 4777 | 7324 | 0,01 | 2388 | 3662 | 0,012 | 1910 | 2929 | 0,015 | |
| Thermoplastic plastics | 15 | 23 | 4777 | 7324 | 0,01 | 2388 | 3662 | 0,012 | 1910 | 2929 | 0,015 | |
| Soft and light wood | 21 | 30 | 6688 | 9554 | 0,012 | 3344 | 4777 | 0,014 | 2675 | 3821 | 0,017 | |
| Compact and hard wood | 18 | 27 | 5732 | 8598 | 0,01 | 2866 | 4299 | 0,013 | 2292 | 3439 | 0,015 | |
| Key | |
| vc = cutting speed [m/min] |  |
| f = feed [mm/r] | |
| n = rotation speed [rpm] | |
| The suggested cutting values are reference values and must be adapted to the respective conditions. | |
| For dia. 10.0-12.5 | |||||||||||||||
| Material designation | Tensile strength | from dia. 10.0 | from dia. 12.5 | ||||||||||||
| ≤ dia. 6 | > dia. 6 | ≤ dia. 6.5 | > dia. 6.5 | ||||||||||||
| vc | n | f | n | f | n | f | n | f | |||||||
| from | to | from | to | from | to | from | to | from | to | ||||||
| General structural steels | ≤ 850 N/mm² | 18 | 27 | 955 | 1433 | 0,027 | 573 | 859 | 0,035 | 881 | 1322 | 0,027 | 458 | 687 | 0,038 |
| Unalloyed hardened steels | ≤ 850 N/mm² | 18 | 27 | 955 | 1433 | 0,027 | 573 | 859 | 0,035 | 881 | 1322 | 0,027 | 458 | 687 | 0,038 |
| Low-alloy hardened steels | ≤ 850 N/mm² | 18 | 27 | 955 | 1433 | 0,027 | 573 | 859 | 0,035 | 881 | 1322 | 0,027 | 458 | 687 | 0,038 |
| Unalloyed hardened steels | ≤ 1,000 N/mm² | 15 | 23 | 796 | 1220 | 0,025 | 477 | 732 | 0,031 | 734 | 1126 | 0,025 | 382 | 585 | 0,035 |
| Low-alloy hardened steels | ≤ 1,000 N/mm² | 15 | 23 | 796 | 1220 | 0,025 | 477 | 732 | 0,031 | 734 | 1126 | 0,025 | 382 | 585 | 0,035 |
| Alloyed hardened steels | ≤ 1,300 N/mm² | 10 | 15 | 530 | 796 | 0,025 | 318 | 477 | 0,031 | 489 | 734 | 0,025 | 254 | 382 | 0,035 |
| Nitriding steels | ≤ 1,300 N/mm² | 10 | 15 | 530 | 796 | 0,025 | 318 | 477 | 0,031 | 489 | 734 | 0,025 | 254 | 382 | 0,035 |
| Tool steels | ≤ 1,300 N/mm² | 10 | 15 | 530 | 796 | 0,025 | 318 | 477 | 0,031 | 489 | 734 | 0,025 | 254 | 382 | 0,035 |
| High-speed steels | ≤ 1,300 N/mm² | 10 | 15 | 530 | 796 | 0,025 | 318 | 477 | 0,031 | 489 | 734 | 0,025 | 254 | 382 | 0,035 |
| Cast iron | ≤ 350 HB | 15 | 23 | 796 | 1220 | 0,025 | 477 | 732 | 0,031 | 734 | 1126 | 0,025 | 382 | 585 | 0,035 |
| Spheroidal graphite and malleable iron | ≤ 350 HB | 15 | 23 | 796 | 1220 | 0,025 | 477 | 732 | 0,031 | 734 | 1126 | 0,025 | 382 | 585 | 0,035 |
| Stainless steels | 1,300 N/mm² | 8 | 12 | 424 | 636 | 0,027 | 254 | 382 | 0,031 | 391 | 587 | 0,027 | 203 | 305 | 0,037 |
| Titanium | 850 N/mm² | 6 | 10 | 318 | 530 | 0,025 | 191 | 318 | 0,031 | 293 | 489 | 0,027 | 153 | 255 | 0,035 |
| Aluminium | ≤ 600 N/mm² | 35 | 45 | 1857 | 2388 | 0,027 | 1114 | 1433 | 0,035 | 1714 | 2204 | 0,027 | 891 | 1146 | 0,038 |
| Thermosetting plastics | 15 | 23 | 796 | 1220 | 0,027 | 477 | 732 | 0,035 | 734 | 1126 | 0,027 | 382 | 585 | 0,038 | |
| Thermoplastic plastics | 15 | 23 | 796 | 1220 | 0,027 | 477 | 732 | 0,035 | 734 | 1126 | 0,027 | 382 | 585 | 0,038 | |
| Soft and light wood | 21 | 30 | 1114 | 1592 | 0,03 | 668 | 955 | 0,038 | 1028 | 1469 | 0,03 | 535 | 764 | 0,041 | |
| Compact and hard wood | 18 | 27 | 955 | 1433 | 0,03 | 573 | 859 | 0,036 | 881 | 1322 | 0,03 | 458 | 687 | 0,038 | |
| For dia. 6.3-8.0 | |||||||||
| Material designation | Tensile strength | from dia. 6.3 | from dia. 8.0 | ||||||
| vc | n | f | n | f | |||||
| from | to | from | to | from | to | ||||
| General structural steels | ≤ 850 N/mm² | 18 | 27 | 909 | 1364 | 0,027 | 716 | 1074 | 0,03 |
| Unalloyed hardened steels | ≤ 850 N/mm² | 18 | 27 | 909 | 1364 | 0,027 | 716 | 1074 | 0,03 |
| Low-alloy hardened steels | ≤ 850 N/mm² | 18 | 27 | 909 | 1364 | 0,027 | 716 | 1074 | 0,03 |
| Unalloyed hardened steels | ≤ 1,000 N/mm² | 15 | 23 | 758 | 1162 | 0,025 | 597 | 915 | 0,028 |
| Low-alloy hardened steels | ≤ 1,000 N/mm² | 15 | 23 | 758 | 1162 | 0,025 | 597 | 915 | 0,028 |
| Alloyed hardened steels | ≤ 1,300 N/mm² | 10 | 15 | 505 | 758 | 0,025 | 398 | 597 | 0,028 |
| Nitriding steels | ≤ 1,300 N/mm² | 10 | 15 | 505 | 758 | 0,025 | 398 | 597 | 0,028 |
| Tool steels | ≤ 1,300 N/mm² | 10 | 15 | 505 | 758 | 0,025 | 398 | 597 | 0,028 |
| High-speed steels | ≤ 1,300 N/mm² | 10 | 15 | 505 | 758 | 0,025 | 398 | 597 | 0,028 |
| Cast iron | ≤ 350 HB | 15 | 23 | 758 | 1162 | 0,025 | 597 | 915 | 0,028 |
| Spheroidal graphite and malleable iron | ≤ 350 HB | 15 | 23 | 758 | 1162 | 0,025 | 597 | 915 | 0,028 |
| Stainless steels | 1,300 N/mm² | 8 | 12 | 404 | 606 | 0,027 | 318 | 477 | 0,03 |
| Titanium | 850 N/mm² | 6 | 10 | 303 | 505 | 0,025 | 239 | 398 | 0,028 |
| Aluminium | ≤ 600 N/mm² | 35 | 45 | 1769 | 2274 | 0,027 | 1393 | 1791 | 0,03 |
| Thermosetting plastics | 15 | 23 | 758 | 1162 | 0,027 | 597 | 915 | 0,03 | |
| Thermoplastic plastics | 15 | 23 | 758 | 1162 | 0,027 | 597 | 915 | 0,03 | |
| Soft and light wood | 21 | 30 | 1061 | 1516 | 0,03 | 836 | 1194 | 0,033 | |
| Compact and hard wood | 18 | 27 | 909 | 1364 | 0,03 | 716 | 1074 | 0,032 | |
| For dia. 3.15-5.0 | ||||||||||||
| Material designation | Tensile strength | from dia. 3.15 | from dia. 4.0 | from dia. 5.0 | ||||||||
| vc | n | f | n | f | n | f | ||||||
| from | to | from | to | from | to | from | to | |||||
| General structural steels | ≤ 850 N/mm² | 18 | 27 | 1819 | 2729 | 0,017 | 1433 | 2149 | 0,02 | 1146 | 1719 | 0,025 |
| Unalloyed hardened steels | ≤ 850 N/mm² | 18 | 27 | 1819 | 2729 | 0,017 | 1433 | 2149 | 0,02 | 1146 | 1719 | 0,025 |
| Low-alloy hardened steels | ≤ 850 N/mm² | 18 | 27 | 1819 | 2729 | 0,017 | 1433 | 2149 | 0,02 | 1146 | 1719 | 0,025 |
| Unalloyed hardened steels | ≤ 1,000 N/mm² | 15 | 23 | 1516 | 2325 | 0,015 | 1194 | 1831 | 0,018 | 955 | 1464 | 0,021 |
| Low-alloy hardened steels | ≤ 1,000 N/mm² | 15 | 23 | 1516 | 2325 | 0,015 | 1194 | 1831 | 0,018 | 955 | 1464 | 0,021 |
| Alloyed hardened steels | ≤ 1,300 N/mm² | 10 | 15 | 1011 | 1516 | 0,015 | 796 | 1194 | 0,018 | 636 | 955 | 0,021 |
| Nitriding steels | ≤ 1,300 N/mm² | 10 | 15 | 1011 | 1516 | 0,015 | 796 | 1194 | 0,018 | 636 | 955 | 0,021 |
| Tool steels | ≤ 1,300 N/mm² | 10 | 15 | 1011 | 1516 | 0,015 | 796 | 1194 | 0,018 | 636 | 955 | 0,021 |
| High-speed steels | ≤ 1,300 N/mm² | 10 | 15 | 1011 | 1516 | 0,015 | 796 | 1194 | 0,018 | 636 | 955 | 0,021 |
| Cast iron | ≤ 350 HB | 15 | 23 | 1516 | 2325 | 0,015 | 1194 | 1831 | 0,018 | 955 | 1464 | 0,021 |
| Spheroidal graphite and malleable iron | ≤ 350 HB | 15 | 23 | 1516 | 2325 | 0,015 | 1194 | 1831 | 0,018 | 955 | 1464 | 0,021 |
| Stainless steels | 1,300 N/mm² | 8 | 12 | 808 | 1213 | 0,017 | 636 | 955 | 0,02 | 509 | 764 | 0,023 |
| Titanium | 850 N/mm² | 6 | 10 | 606 | 1011 | 0,015 | 477 | 796 | 0,018 | 382 | 637 | 0,021 |
| Aluminium | ≤ 600 N/mm² | 35 | 45 | 3538 | 4549 | 0,016 | 2786 | 3582 | 0,02 | 2229 | 2866 | 0,025 |
| Thermosetting plastics | 15 | 23 | 1516 | 2325 | 0,016 | 1194 | 1831 | 0,02 | 955 | 1464 | 0,025 | |
| Thermoplastic plastics | 15 | 23 | 1516 | 2325 | 0,016 | 1194 | 1831 | 0,02 | 955 | 1464 | 0,025 | |
| Soft and light wood | 21 | 30 | 2123 | 3033 | 0,018 | 1672 | 2388 | 0,023 | 1338 | 1910 | 0,028 | |
| Compact and hard wood | 18 | 27 | 1819 | 2729 | 0,018 | 1433 | 2149 | 0,022 | 1146 | 1719 | 0,027 | |
Last viewed

W-CONNECT module with Bluetooth function

Brush seal for ABILIT 50-G and ABILIT 120-G interior sliding door fitting

Hexagonal bolt with shank ISO 4014, zinc plated 8.8 steel with thick-layer passivation (VZD)

Weld-in bulkhead fitting ISO 8434-1, stainless steel 1.4571
Low-cut safety shoes, S3 Steitz CP 4340 SF
Safety shoes, S1P Steitz VD PRO 1100 SF

Hexagon bolt with shank DIN 601/ISO 4016, steel 4.8, zinc-plated, blue passivated (A2K), with nut

Work jacket

Low-cut safety shoes, S2 Steitz CP 4300 ESD
TRIATHLON Power engine oil 5W-40