


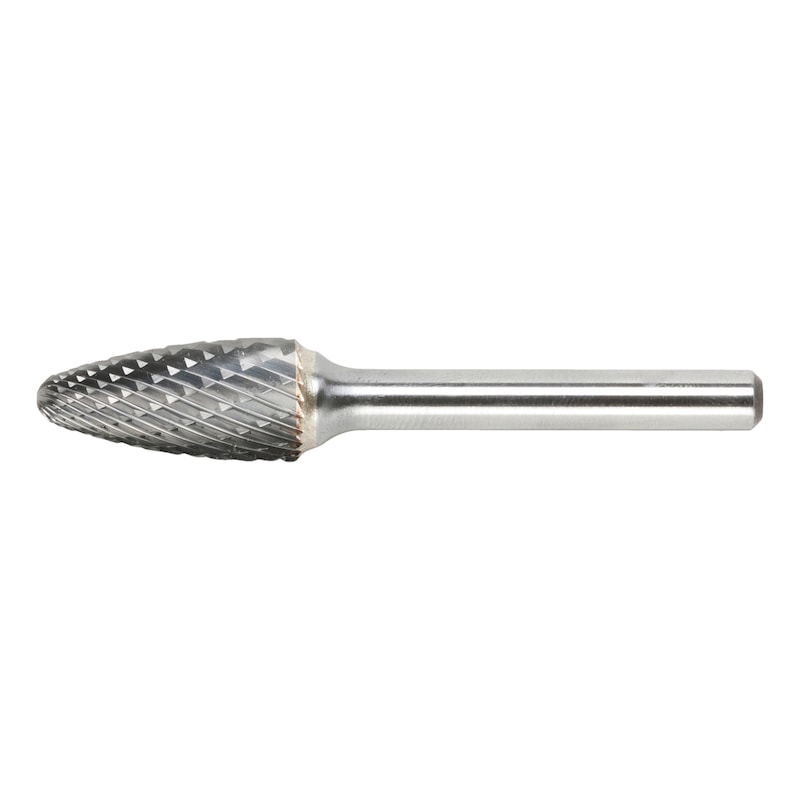

Tungsten carbide bur with MX teeth
MILBIT-CYL-TC-RBF-MX-D8-WL20MM
Art.-no. 0616004021
EAN 4053478099799

Register now and access more than 125,000 products
Datasheets(X)

Deburring, working contours, surface machining, weld seam processing, shaping, chamfering/rounding edges
Form | Semicircular shape |
Head diameter x cutting edge length | 8 x 20 mm |
Length | 65 mm |
Shank diameter | 6 mm |
Material to be processed | Steel, Cast metal, Stainless steel, Special alloy, Hard and tough material, Non-ferrous metal |
Suitable for hardnesses up to | 60 HRC |
Quality | Würth-Standard |
Teeth type | MX |
Cutting material | Carbide |
Surface | Plain |
Service life (points system) | 2 of 4 points |
Cutting efficiency (point system) | 2 of 4 points |
Surface quality/finish (points system) | 2 of 4 points |
Versatility (points system) | 3 of 4 points |
Guiding behaviour (point system) | 2 of 4 points |
Shank style | Cylindrical |
| Cutting values | ||||||||||||
| For dia. 3.0-8.0 | ||||||||||||
| Material designation | Tensile strength | Dia. 3.0 | Dia. 6.0 | Dia. 8.0 | ||||||||
| vc | n | f | n | f | n | f | ||||||
| from | to | from | to | from | to | from | to | |||||
| Steels | ||||||||||||
| General structural steels | ≤ 850 N/mm² | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| Unalloyed quenched and tempered steels | ≤ 850 N/mm² | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| Low-alloy quenched and tempered steels | ≤ 850 N/mm² | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| Unalloyed quenched and tempered steels | ≤ 1,000 N/mm² | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| Low-alloy quenched and tempered steels | ≤ 1,000 N/mm² | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| Alloyed quenched and tempered steels | ≤ 1,200 N/mm² | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| Nitriding steels | ≤ 1,200 N/mm² | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| Tool steels | ≤ 1,200 N/mm² | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| High-speed steels | ≤ 1,200 N/mm² | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| Stainless steels | ||||||||||||
| Stainless steels | ≤ 850 N/mm² | 250 | 350 | 27000 | 37000 | 9 | 13000 | 19000 | 18,5 | 10000 | 14000 | 25 |
| Sulphurated stainless steel | ≤ 850 N/mm² | 250 | 350 | 27000 | 37000 | 9 | 13000 | 19000 | 18,5 | 10000 | 14000 | 25 |
| Austenitic stainless steel | ≤ 850 N/mm² | 250 | 350 | 27000 | 37000 | 9 | 13000 | 19000 | 18,5 | 10000 | 14000 | 25 |
| Martensitic stainless steel | ≤ 850 N/mm² | 250 | 350 | 27000 | 48000 | 9 | 13000 | 19000 | 18,5 | 10000 | 14000 | 25 |
| Special alloys | ≤ 1,200 N/mm² | 250 | 450 | 27000 | 48000 | 9 | 13000 | 24000 | 18,5 | 10000 | 18000 | 25 |
| Cast metals | ||||||||||||
| Cast iron | ≤ 350 HB | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| Spheroidal graphite and malleable iron, chilled cast iron | ≤ 350 HB | 450 | 600 | 48000 | 64000 | 9 | 24000 | 32000 | 18 | 18000 | 24000 | 25 |
| Hard materials | ||||||||||||
| Hardox | ≤ 1,400 N/mm² | 250 | 350 | 27000 | 37000 | 9 | 13000 | 19000 | 18,5 | 10000 | 14000 | 25 |
| Spring steels | ≤ 1,100 N/mm² | 250 | 350 | 27000 | 37000 | 9 | 13000 | 19000 | 18,5 | 10000 | 14000 | 25 |
| Non-ferrous metals | ||||||||||||
| Aluminium cast alloys >10 % Si | ≤ 600 N/mm² | 250 | 350 | 27000 | 37000 | 9 | 13000 | 19000 | 18,5 | 10000 | 14000 | 25 |
| Magnesium alloys | ≤ 450 N/mm² | 250 | 450 | 27000 | 48000 | 9 | 13000 | 24000 | 18,5 | 10000 | 18000 | 25 |
| Short-chipping bronze | ≤ 850 N/mm² | 600 | 900 | 64000 | 95000 | 9 | 32000 | 48000 | 18 | 24000 | 36000 | 25 |
| Long-chipping bronze | ≤ 1,000 N/mm² | 600 | 900 | 64000 | 95000 | 9 | 32000 | 48000 | 18 | 24000 | 36000 | 25 |
| Key |
| vc = cutting speed [m/min] |
| f = feed [mm/r] |
| n = rotation speed [rpm] |
| The suggested cutting values are reference values and must be adapted to the respective conditions. |
| For dia. 10.0-12.0 | |||||||||
| Material designation | Tensile strength | Dia. 10.0 | Dia. 12.0 | ||||||
| vc | n | f | n | f | |||||
| from | to | from | to | from | to | ||||
| Steels | |||||||||
| General structural steels | ≤ 850 N/mm² | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| Unalloyed quenched and tempered steels | ≤ 850 N/mm² | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| Low-alloy quenched and tempered steels | ≤ 850 N/mm² | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| Unalloyed quenched and tempered steels | ≤ 1,000 N/mm² | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| Low-alloy quenched and tempered steels | ≤ 1,000 N/mm² | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| Alloyed quenched and tempered steels | ≤ 1,200 N/mm² | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| Nitriding steels | ≤ 1,200 N/mm² | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| Tool steels | ≤ 1,200 N/mm² | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| High-speed steels | ≤ 1,200 N/mm² | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| Stainless steels | |||||||||
| Stainless steels | ≤ 850 N/mm² | 250 | 350 | 8000 | 11000 | 31 | 7000 | 9000 | 36,5 |
| Sulphurated stainless steel | ≤ 850 N/mm² | 250 | 350 | 8000 | 11000 | 31 | 7000 | 9000 | 36,5 |
| Austenitic stainless steel | ≤ 850 N/mm² | 250 | 350 | 8000 | 11000 | 31 | 7000 | 9000 | 36,5 |
| Martensitic stainless steel | ≤ 850 N/mm² | 250 | 350 | 8000 | 11000 | 31 | 7000 | 9000 | 36,5 |
| Special alloys | ≤ 1,200 N/mm² | 250 | 450 | 8000 | 14000 | 31,5 | 7000 | 12000 | 36 |
| Cast metals | |||||||||
| Cast iron | ≤ 350 HB | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| Spheroidal graphite and malleable iron, chilled cast iron | ≤ 350 HB | 450 | 600 | 14000 | 19000 | 31,5 | 12000 | 16000 | 37 |
| Hard materials | |||||||||
| Hardox | ≤ 1,400 N/mm² | 250 | 350 | 8000 | 11000 | 31 | 7000 | 9000 | 36,5 |
| Spring steels | ≤ 1,100 N/mm² | 250 | 350 | 8000 | 11000 | 31 | 7000 | 9000 | 36,5 |
| Non-ferrous metals | |||||||||
| Aluminium cast alloys >10 % Si | ≤ 600 N/mm² | 250 | 350 | 8000 | 11000 | 31 | 7000 | 9000 | 36,5 |
| Magnesium alloys | ≤ 450 N/mm² | 250 | 450 | 8000 | 14000 | 31,5 | 7000 | 12000 | 36 |
| Short-chipping bronze | ≤ 850 N/mm² | 600 | 900 | 19000 | 29000 | 31 | 16000 | 24000 | 37 |
| Long-chipping bronze | ≤ 1,000 N/mm² | 600 | 900 | 19000 | 29000 | 31 | 16000 | 24000 | 37 |
Last viewed

Corner joint with cover

Adapter profile 30 SR For single-leaf hold-open devices (ERA)

Spyhole, type B With crystalline lens and 200° viewing angle
Lanyard WAPS

Counter nut, polyamide Metric according to EN 60423

Countersunk washer/washer, deep zinc plated blue

Half-head strip nail, 34°, with ring-shaped shaft steel, plain

Hexagon bolt with thread up to the head DIN 933, A4 stainless steel, plain

Lock washer VS Spring steel, plain

Shutter hinge